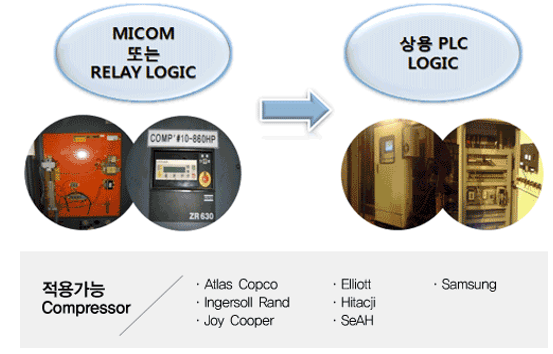
Integrated HMI & SCADA Systems
Integrated HMI & SCADA System
We design and build everything from a small system monitoring a single unit to system integration that ties multiple plants together. The same architecture scales from 100 I/O to 100,000 I/O, and the PLC and HMI are selected to suit site conditions and budget.
The hardest case when introducing a new automation system is when the scale is uncertain.
Today you only need to watch one unit in the test building, but next year the whole line has to be tied together, and rebuilding the system from scratch at that point is all too common.
GENEQ does not lock in just one part of the picture. We lay out the architecture with expansion in mind from the start.
Starting from small-scale monitoring of a single unit, the same framework grows all the way to system integration across multiple plants and complex facilities.
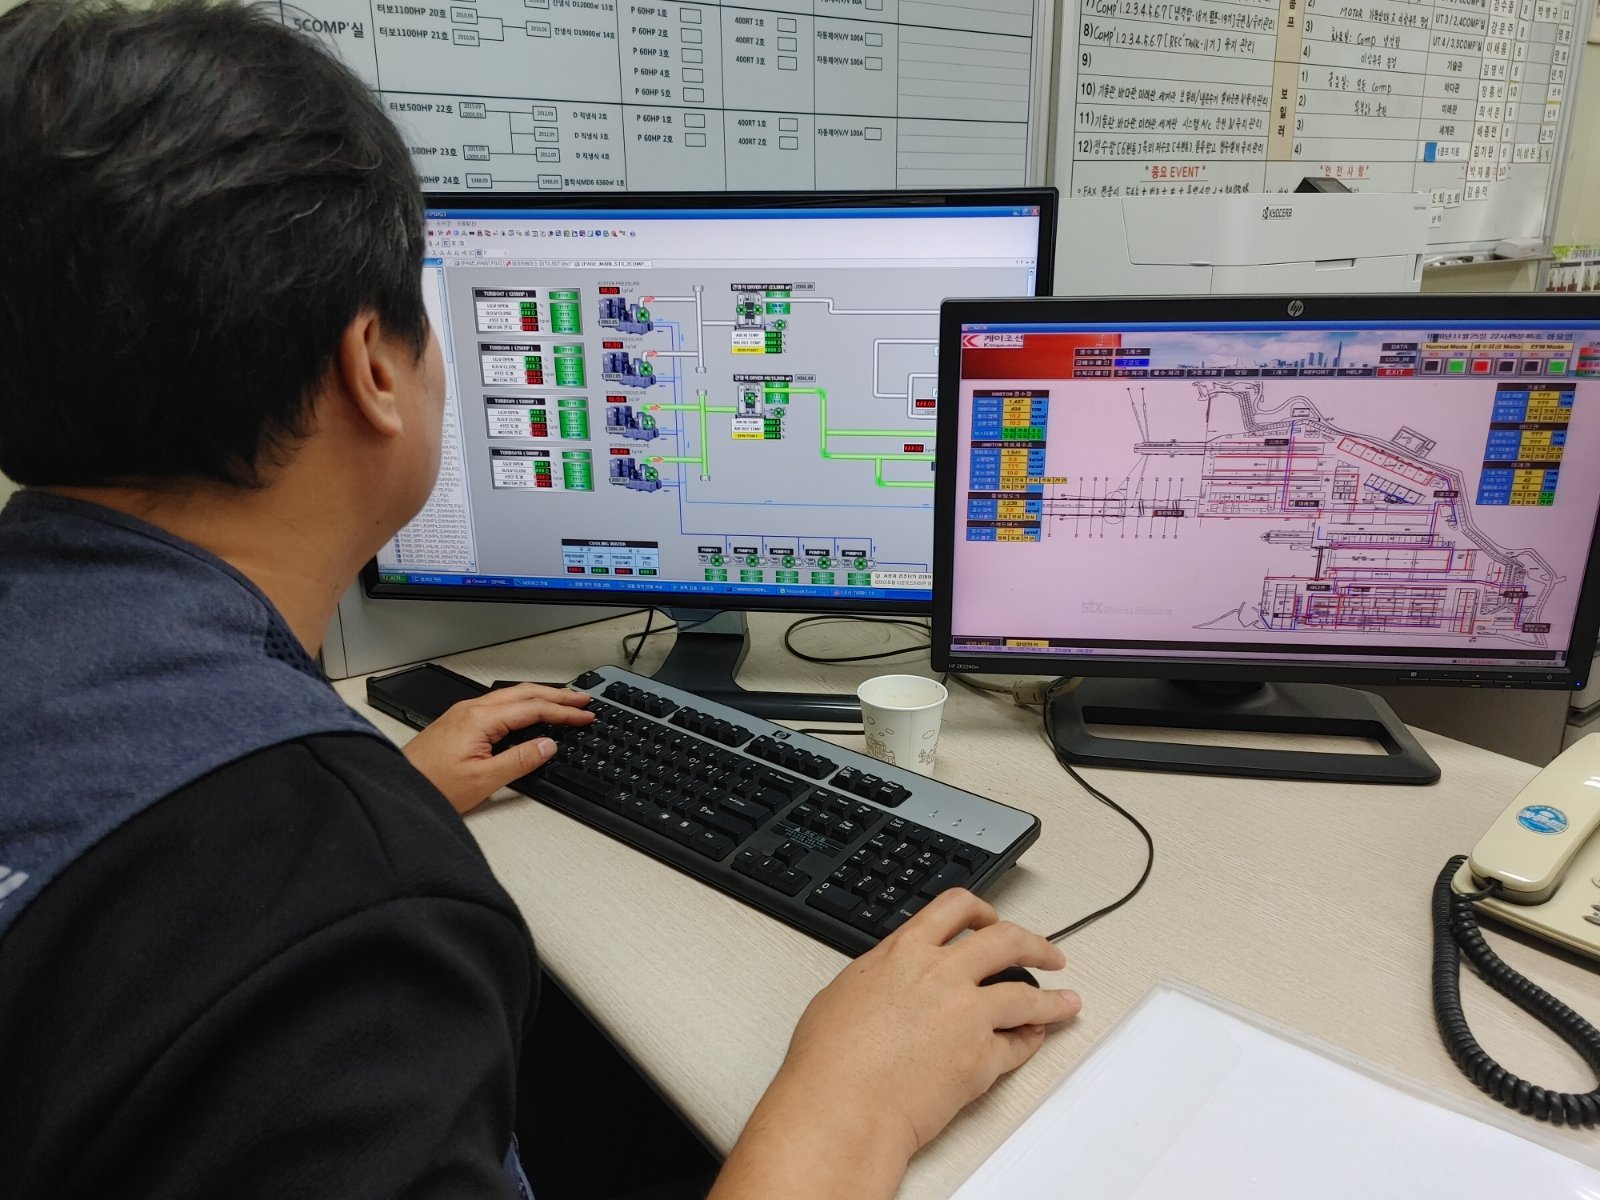
The structure stays the same as the scale grows
Stage | Target | Configuration | Approximate scale |
|---|---|---|---|
Test building · pilot plant | Single-unit monitoring | 1 PC + 1 PLC set, local touch panel | Around 100 I/O |
Production plant | Line-level integrated monitoring and control | Operator stations + distributed PLCs, networked | Several thousand I/O |
Multiple production facilities | Inter-plant integration (SI) | Supervisory SCADA + per-plant subsystems | Up to 100,000 I/O |
When equipment is added, we attach it to the existing structure instead of creating new screens and tags. A system that started at 100 I/O simply grows in place.
Blocking expansion to save on the initial build only costs more at the second round of investment.
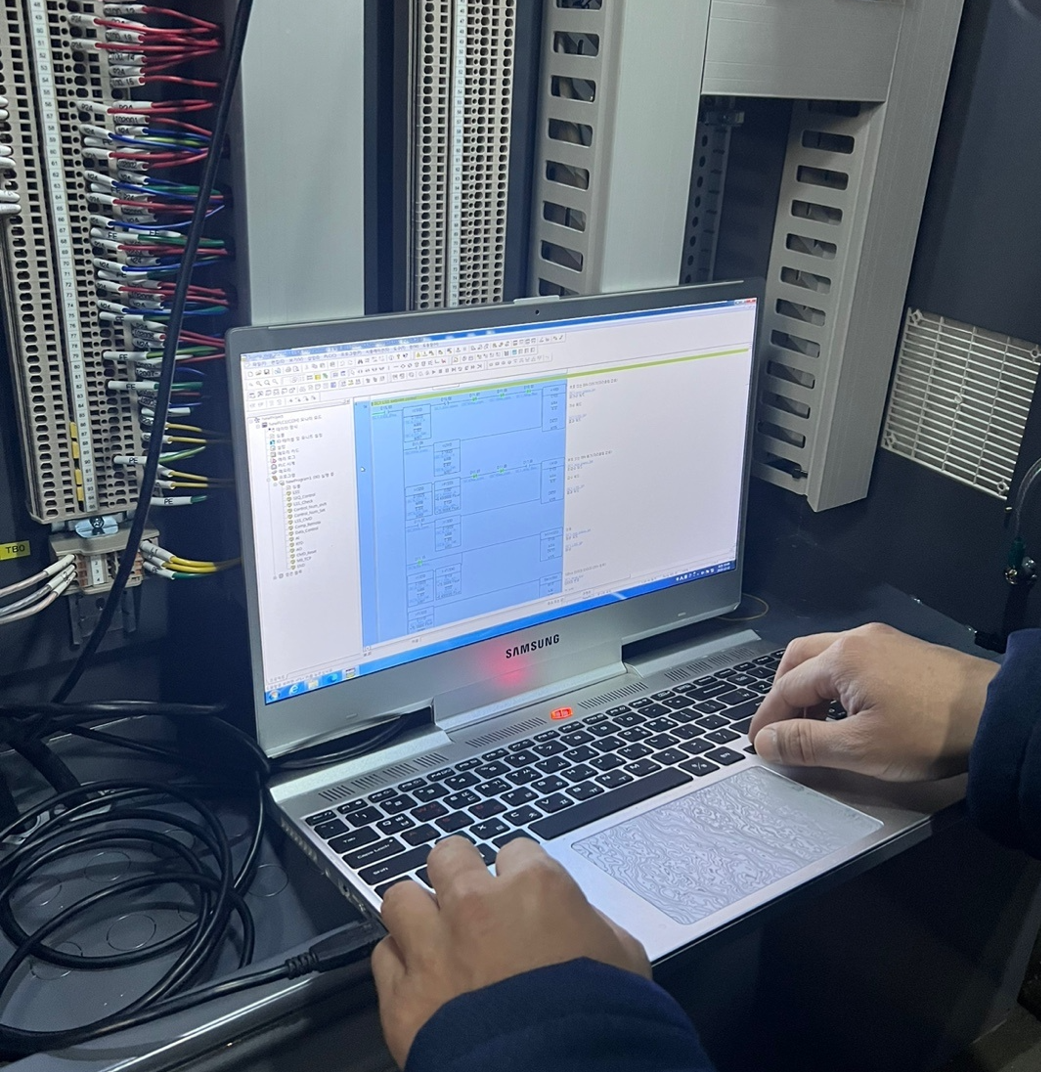
Where it is used
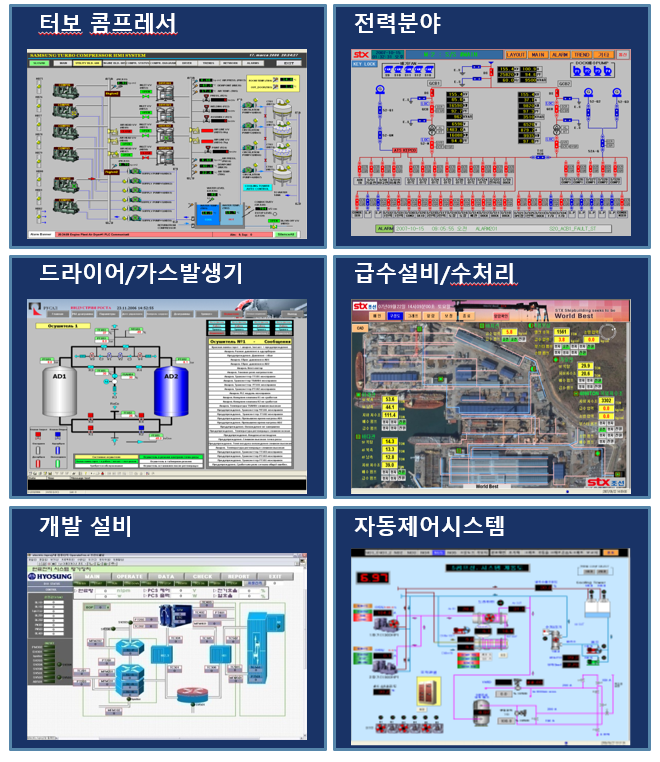
Application | What you see on screen |
|---|---|
Turbo compressors | Operating status per unit, discharge pressure and temperature, load ratio, alarm history |
Power systems | Power distribution single-line diagram, breaker status, voltage, current and energy |
Dryers · gas generators | Adsorption tower changeover status, dew point, regeneration heater and blower operation |
Water supply · water treatment | Pump and valve status, level, flow and water quality, system flow |
Development · test facilities | Test condition setting, real-time acquisition and logging of measurement data |
Process automation | Overall process diagram, interlocks, auto/manual changeover |
Hardware and software
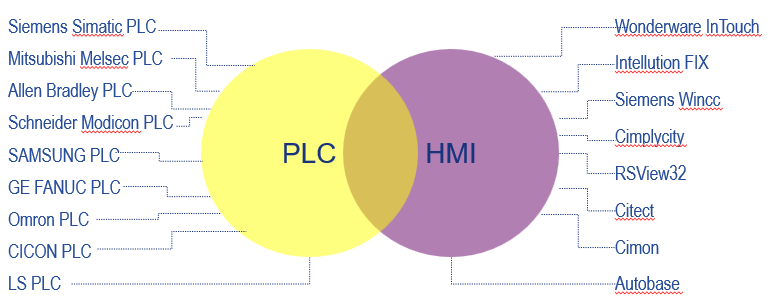
We do not insist on a particular brand. If the plant already uses a PLC family, staying with it is better for parts supply and maintenance; for new facilities we choose based on budget and delivery. We work with proven global brands and cost-effective Korean products alike.
PLC | HMI · SCADA |
|---|---|
Siemens Simatic · Mitsubishi Melsec · Allen-Bradley · Schneider Modicon · SAMSUNG · GE FANUC · Omron · CICON · LS | Wonderware InTouch · Intellution FIX · Siemens WinCC · Cimplicity · RSView32 · Citect · Cimon · Autobase |
How a project proceeds
Stage | What we do |
|---|---|
1. Site survey | Check the equipment list, instrument specifications, and the condition of existing wiring and panels |
2. I/O list · configuration diagram | Fix the signal count and network configuration. This is where scale and quotation are determined |
3. Logic · screen design | Lay out screens in the order operators actually use them |
4. Panel fabrication · wiring | Control panels are designed and built in-house |
5. Factory acceptance test (FAT) | Verify interlocks and alarms with real signals applied |
6. Installation · commissioning | Agree the available shutdown windows in advance and split the schedule accordingly |
7. Handover | Training on screen operation, alarm response and data backup, plus documentation delivery |
Load sharing, which automatically allocates multiple compressors by pressure to reduce unloaded running, is handled as a separate system.
See the "Air Compressor Load Sharing System (LSS)" page.